

In the unforgiving landscape of the mining and quarrying industries, equipment reliability is not merely a performance metric; it is the foundation of profitability. Mining operations often take place in remote mountains, deserts, or thousands of meters underground. In these isolated environments, machinery such as crushers, vibrating screens, and conveyors operates continuously. When a critical component fails, the resulting non-planned downtime can lead to catastrophic financial losses. At the heart of these massive machines are the bearings, tasked with supporting extreme loads, shock impacts, and relentless vibrations.
To meet these severe demands, modern heavy-duty bearings have evolved far beyond standard industrial designs. Today’s mining-grade bearings integrate advanced material engineering, innovative structural designs, and specialized lubrication technologies to ensure uninterrupted operation in the harshest conditions on Earth.
Engineering for the Extreme: Design and Material Innovations
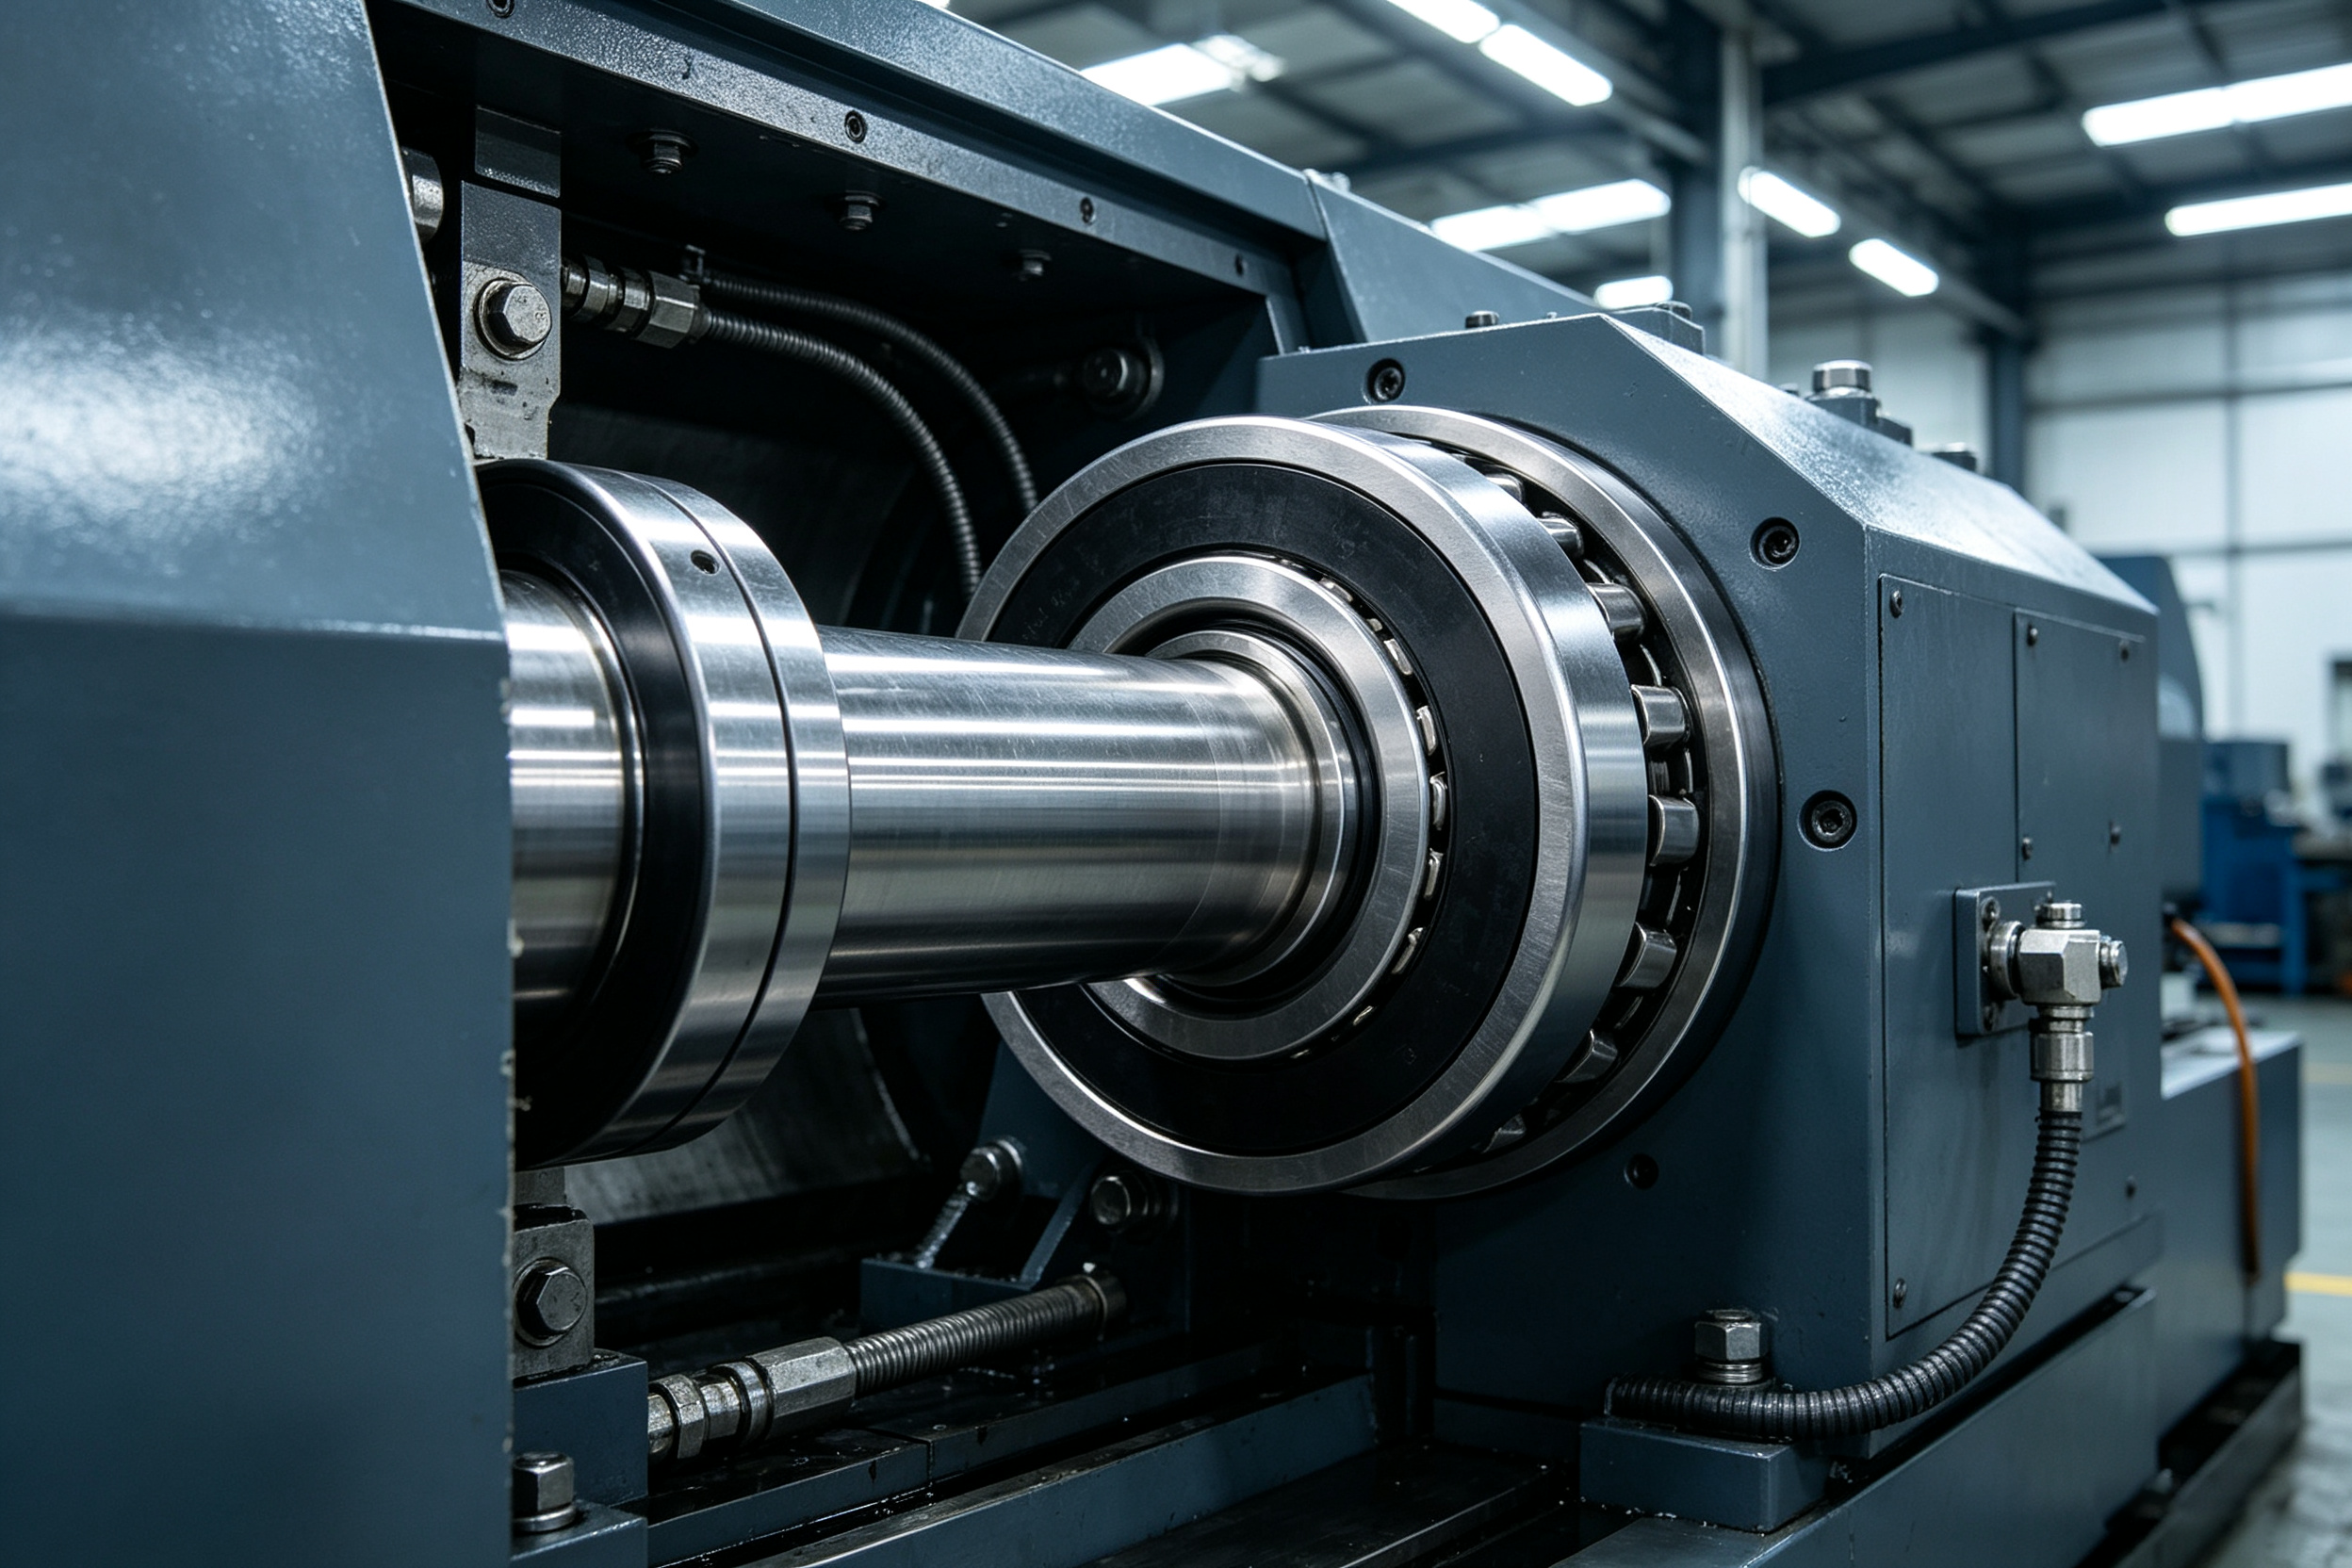
Standard bearings are designed for predictable environments. Mining bearings, however, are engineered to survive chaos. The primary threats in mining are high dynamic loads, severe misalignment, and abrasive contamination. To combat this, leading manufacturers have developed specialized product lines, such as vibrating screen spherical roller bearings and cylindrical roller bearings, which feature significant structural upgrades.
A critical innovation is the use of heavy-duty, precision-machined one-piece brass cages. Unlike standard pressed steel cages, machined brass cages offer superior strength and rigidity under vibrating conditions. They feature contoured roller pockets and special profiling that guide rollers smoothly, reducing stress concentrations and preventing damage caused by slippage, surface fatigue, and flaking.
Furthermore, material science plays a pivotal role. Bearings are now manufactured from ultra-clean, high-strength steel to maximize fatigue strength. Advanced heat treatments, such as special carburizing or nitriding processes, are applied to rollers and rings to prevent cracks from shock loads and enhance resistance to surface wear. Some advanced bearings even feature welded bi-metallic deflectors on the cage, a patented technology that physically blocks abrasive dust and mud from entering the bearing interior, fundamentally solving contamination issues.
| Key Design Feature | Function in Mining Environment | Operational Benefit |
|---|---|---|
| Machined Brass Cage | Guides rollers smoothly and withstands high vibration | Reduces surface fatigue, flaking, and cage breakage |
| Special Heat Treatment | Enhances roller and ring toughness | Prevents cracking from shock loads and impacts |
| Ultra-Clean Steel | Maximizes internal material purity | Significantly increases fatigue life under heavy loads |
| Bi-Metallic Deflectors | Blocks external contaminants (dust/mud) | Prevents internal wear and extends relubrication intervals |
The Role of Advanced Lubrication in Shock Absorption
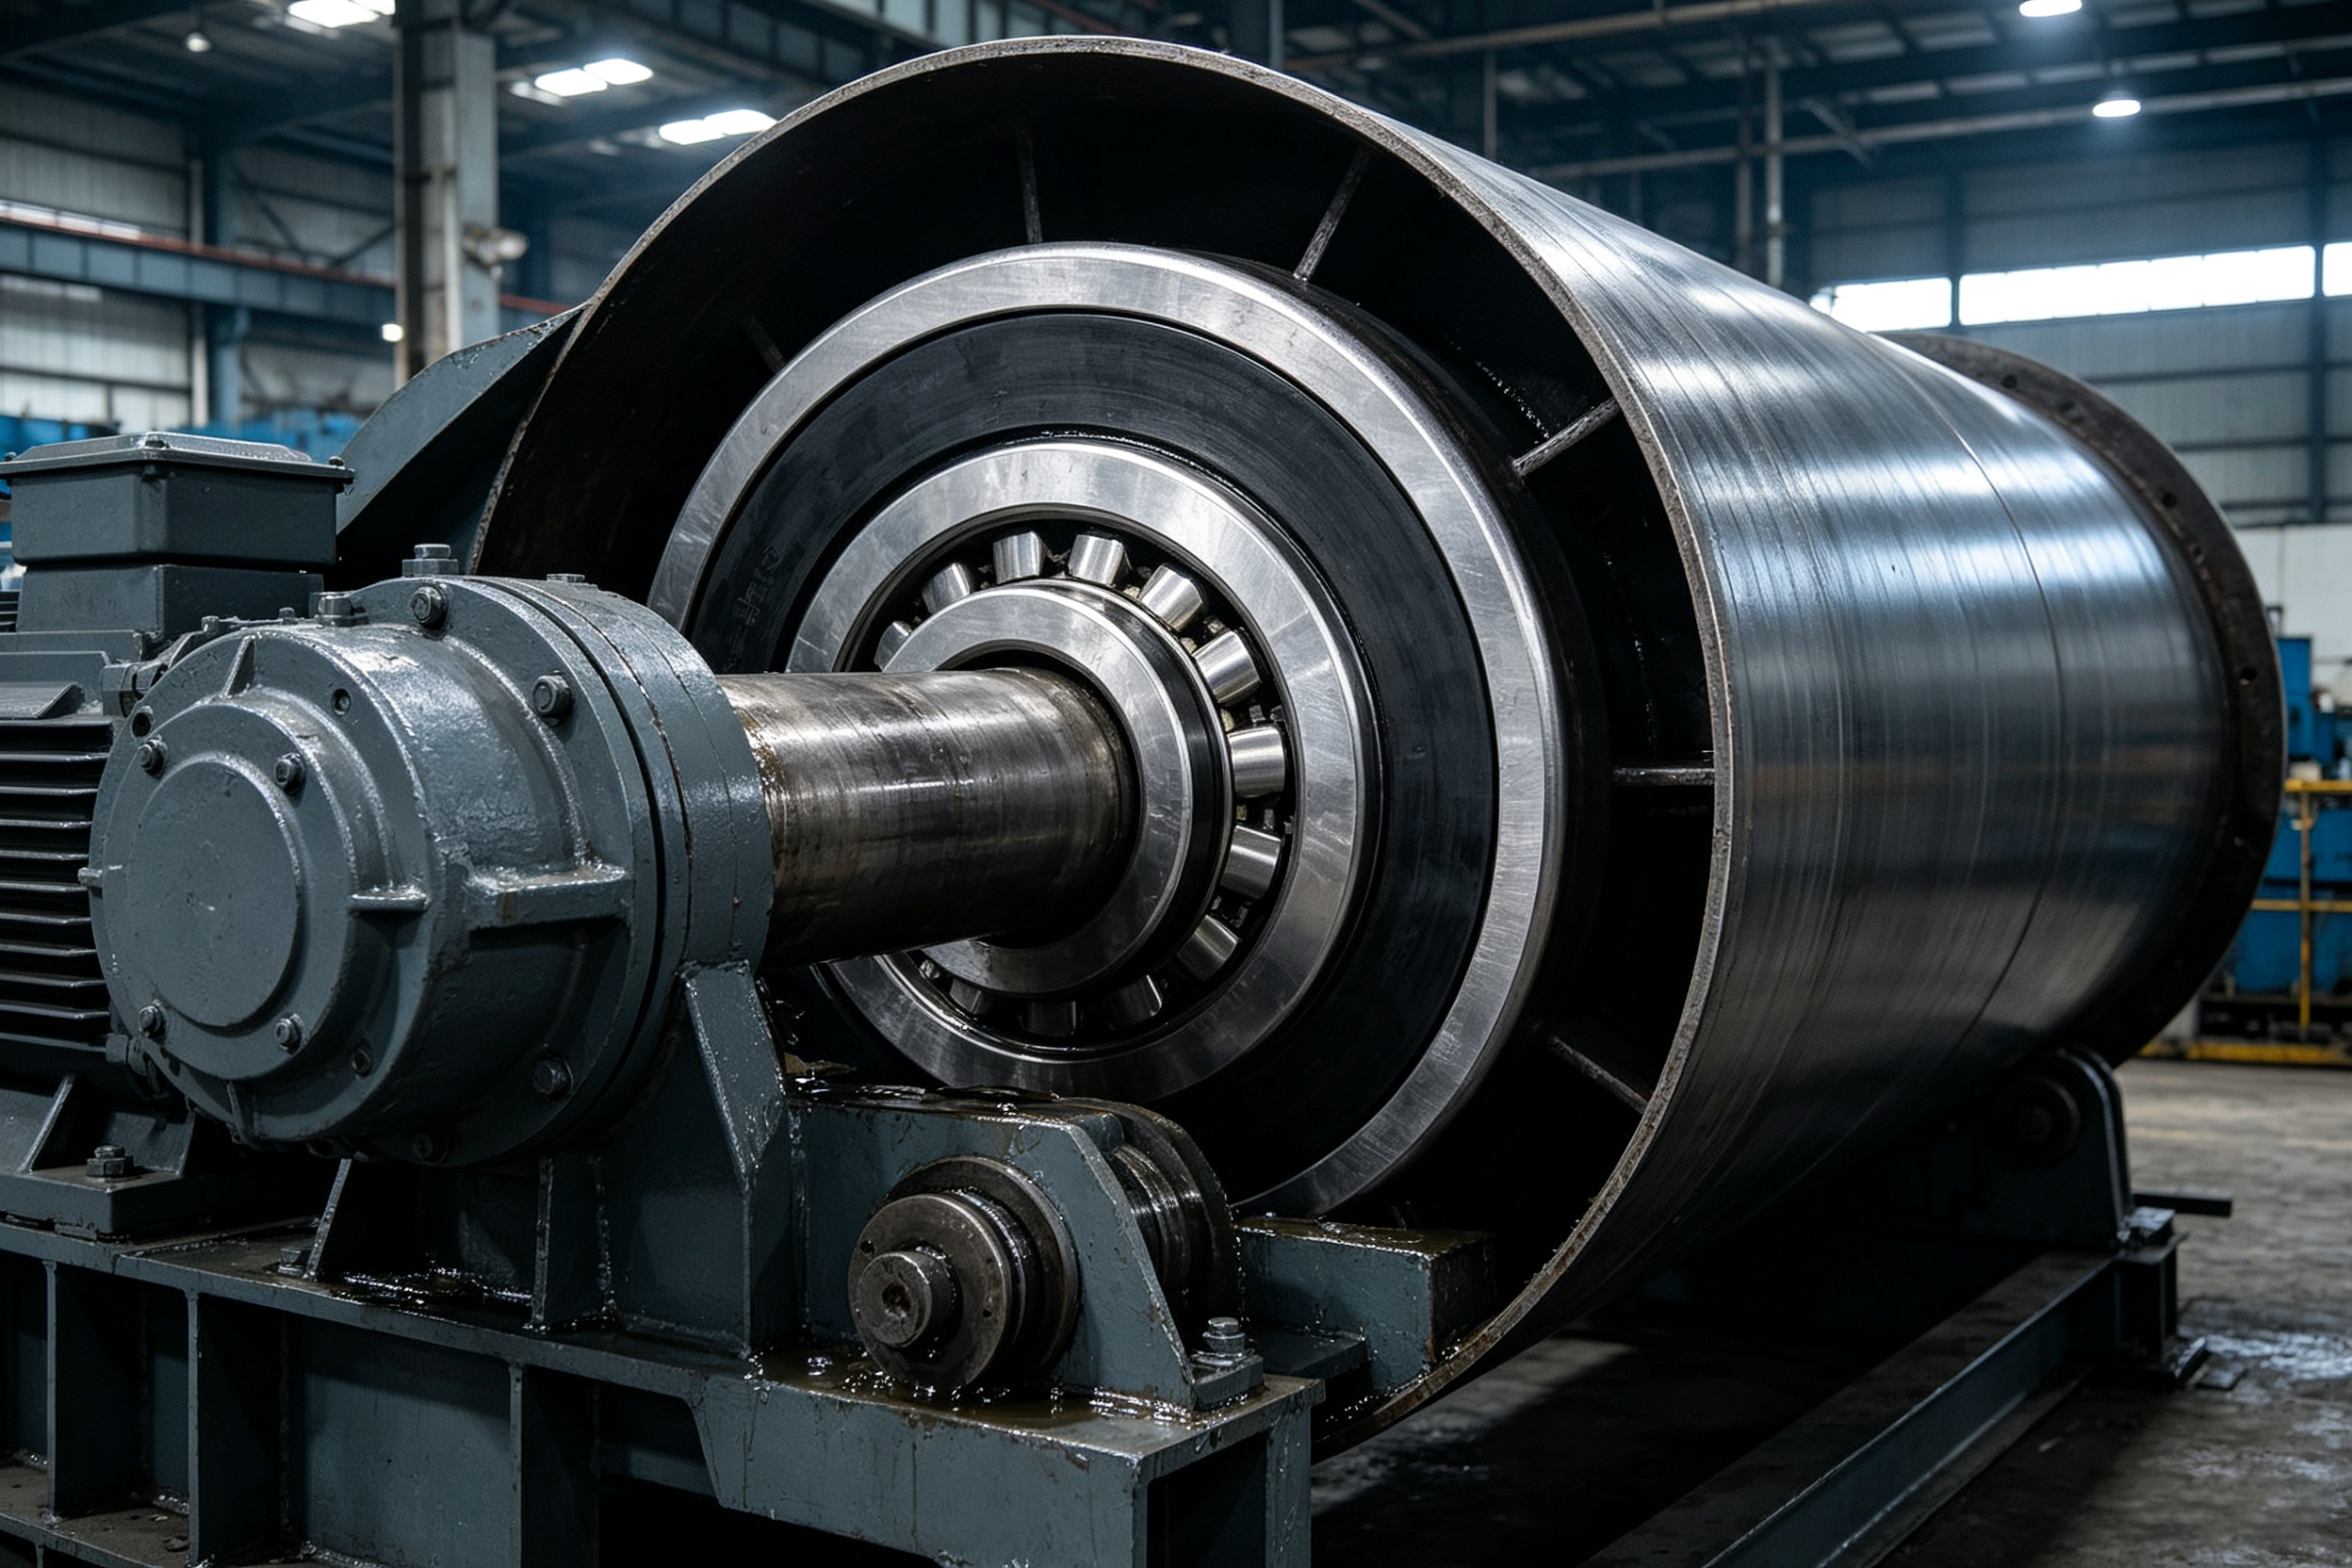
Even the most robust bearing will fail prematurely if the lubrication is inadequate. In mining, bearings face extreme instantaneous contact pressures that can rupture standard oil films. Therefore, selecting the right lubricant is as critical as selecting the bearing itself.
Heavy-duty mining applications require lubricants with high base oil viscosity and extreme pressure (EP) additives. These EP additives form a resilient chemical保护膜 (protective film) on the metal surfaces, preventing direct metal-to-metal contact during severe shock events. Additionally, modern sealed spherical roller bearings are being developed with specialized grease formulations that sustain oil film thickness even under differential sliding conditions, achieving up to ten times the abrasion resistance of conventional greases.
| Lubricant Type | Key Characteristics | Ideal Mining Application |
|---|---|---|
| Complex Lithium EP Grease | High load capacity, excellent water resistance | General heavy-duty mining conveyors and crushers |
| Calcium Sulfonate Grease | Natural extreme pressure, high-temperature stability | Wet environments, rolling mills, continuous casters |
| Solid-Lubricant Enhanced Grease | Contains solid lubricants for boundary protection | Low-speed, ultra-high shock load applications |
| Anti-Abrasion Specialty Grease | Sustains oil film under differential sliding | Sealed vibrating screens and shakers |
Real-World Impact: Extending Service Life and Reducing Costs
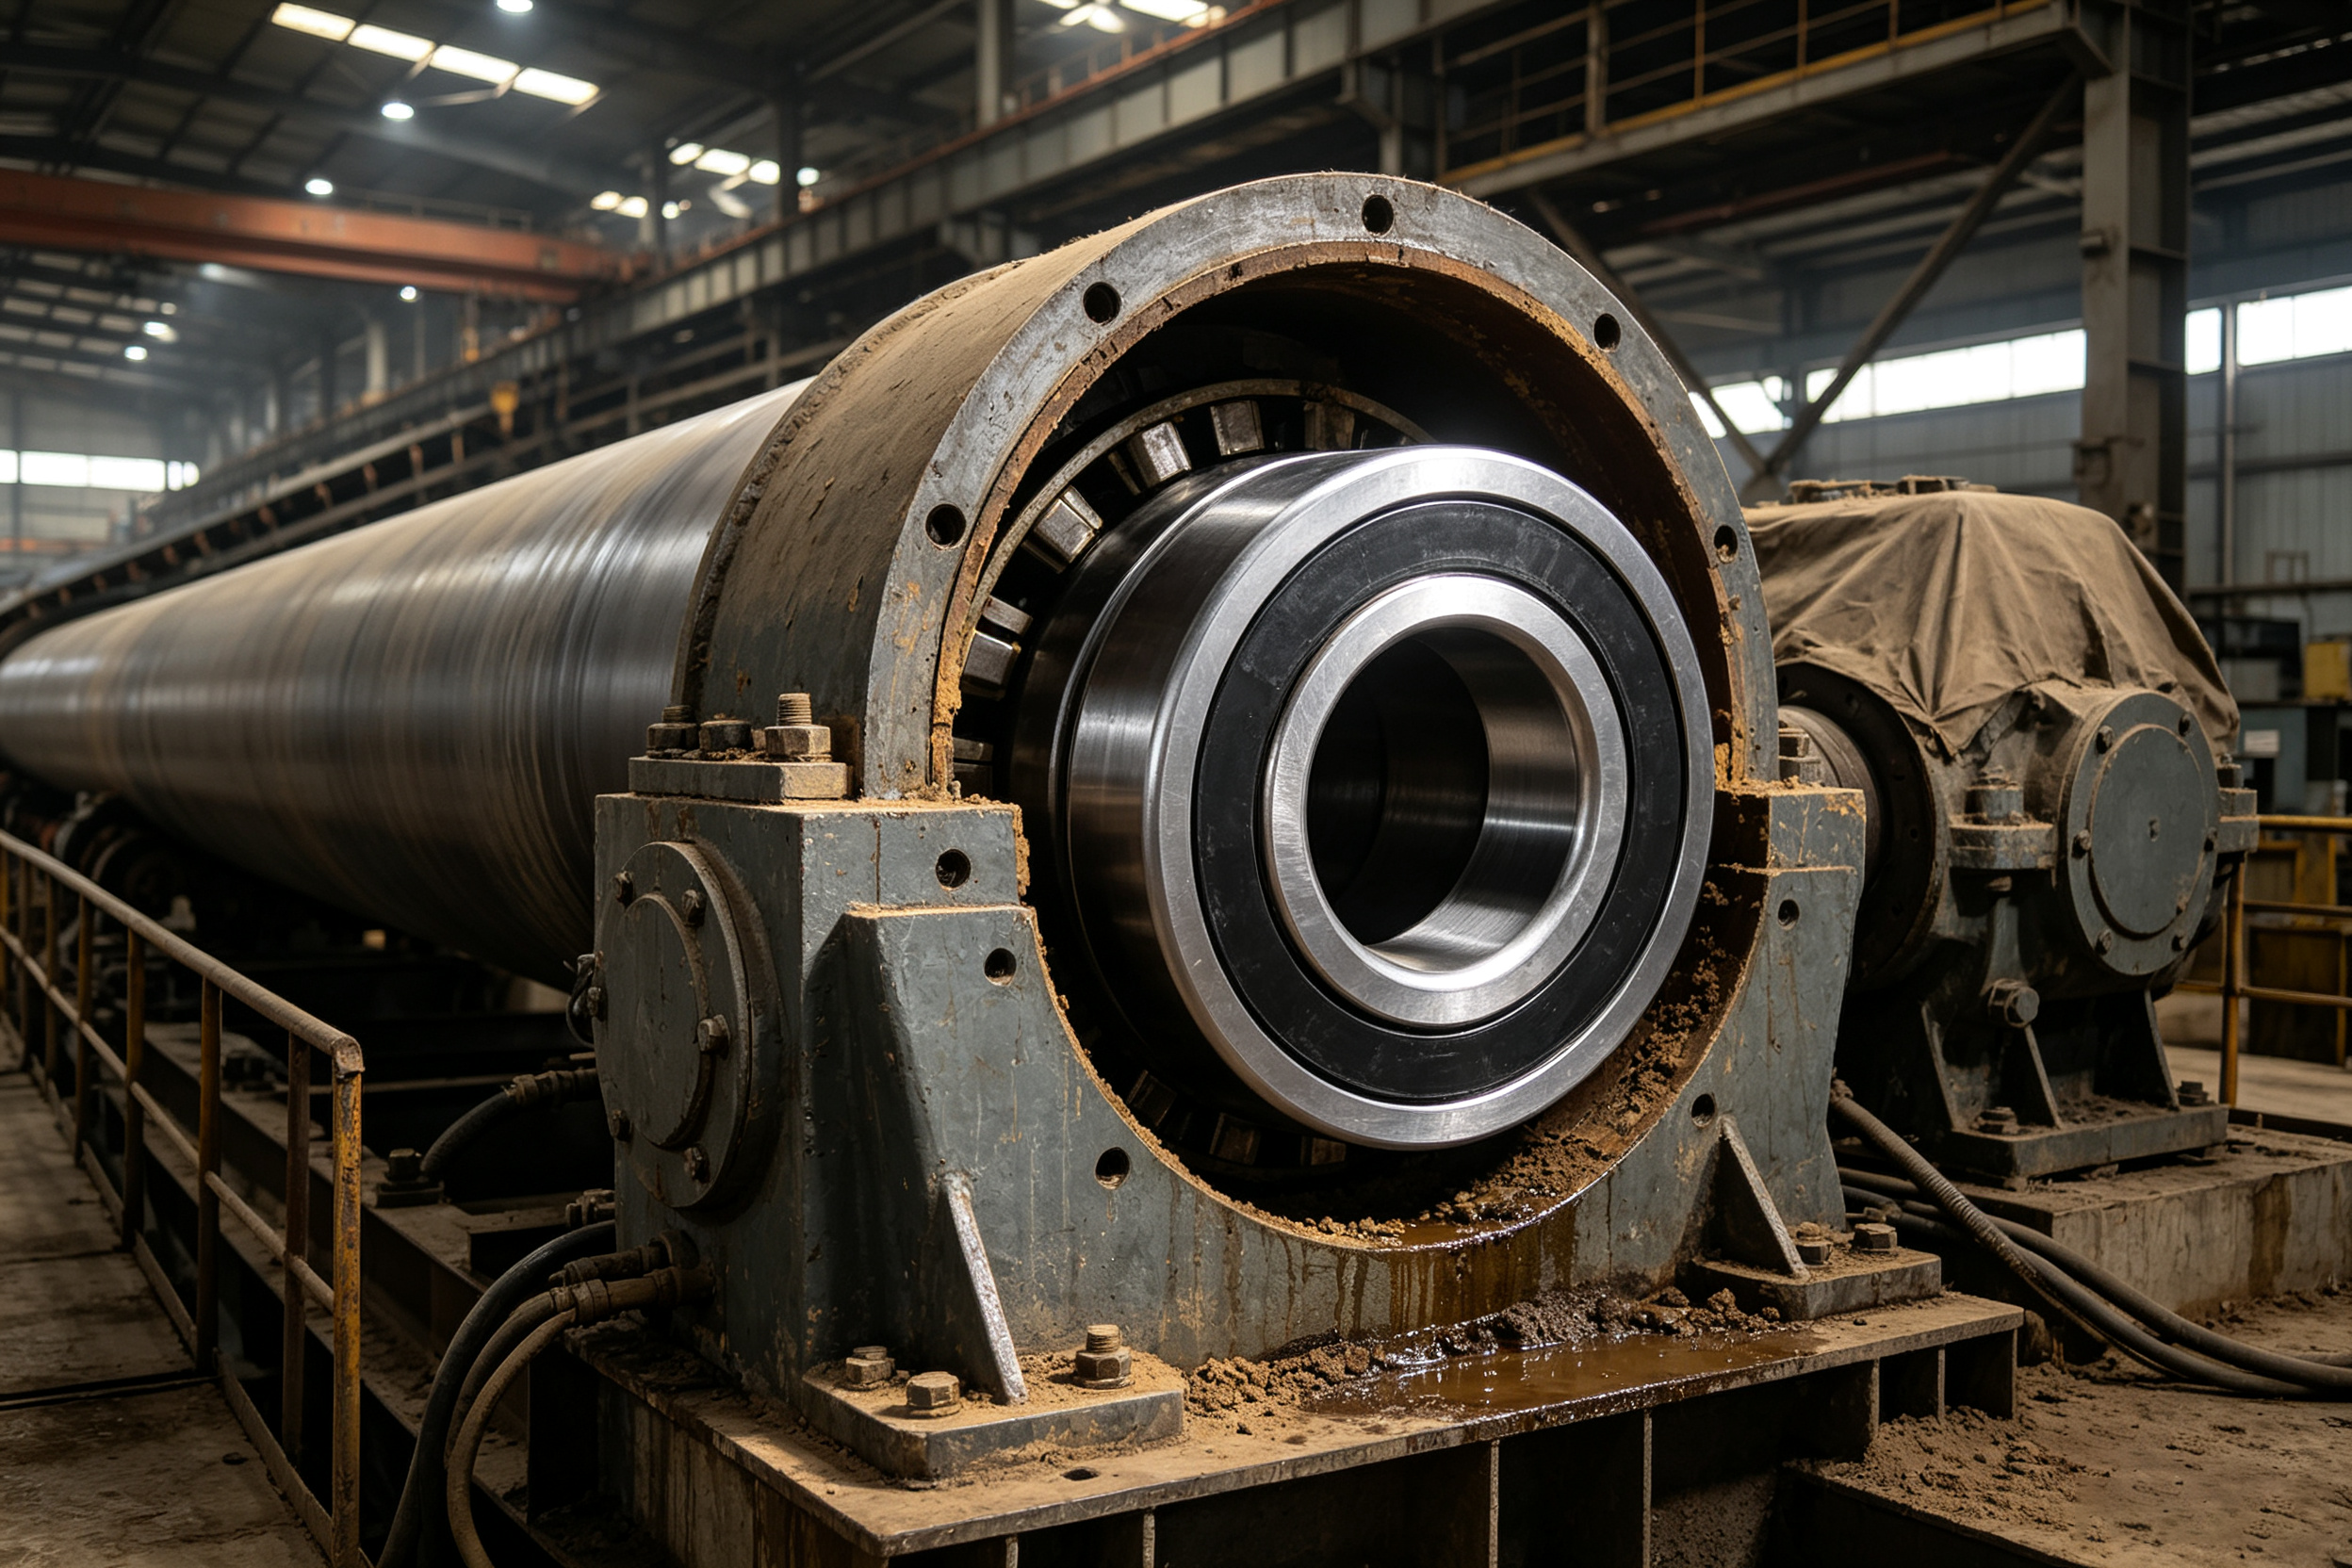
The ultimate test of any mining bearing is its performance in the field. The integration of optimized internal clearances, superior roller guidance, and advanced materials translates directly to measurable operational improvements. Field tests in harsh quarry environments have demonstrated that next-generation bearings can extend service life by up to five times compared to standard solutions.
This extended longevity dramatically reduces maintenance costs and non-planned downtime. For example, in high-humidity, abrasive limestone dust environments, facilities utilizing advanced sealed bearings have reported reducing annual downtime from six instances to just one, resulting in significant net revenue increases. Furthermore, improved grease retention capabilities can reduce relubrication frequency by more than half, lowering both labor costs and environmental impact.
As mining operations push deeper and equipment scales up, the demand for specialized, heavy-duty reliability will only intensify. By investing in bearings engineered specifically for extreme vibrations and shock loads, mining companies can transform a traditional vulnerability into a strategic advantage, ensuring that their most critical assets keep turning, no matter the conditions.
Frequently Asked Questions (FAQ)
Q: Why do standard bearings fail in mining environments?
A: Standard bearings lack the heavy-duty cages, specialized heat treatments, and superior sealing required to withstand extreme shock loads, high vibrations, and abrasive dust found in mining.
A: Standard bearings lack the heavy-duty cages, specialized heat treatments, and superior sealing required to withstand extreme shock loads, high vibrations, and abrasive dust found in mining.
Q: How do machined brass cages improve bearing reliability?
A: They provide superior strength and rigidity under severe vibrations, guiding rollers smoothly to prevent stress concentrations, surface fatigue, and premature cage breakage.
A: They provide superior strength and rigidity under severe vibrations, guiding rollers smoothly to prevent stress concentrations, surface fatigue, and premature cage breakage.
Q: What makes mining-grade lubricants different from standard greases?
A: They contain extreme pressure (EP) additives and high base oil viscosity to form a resilient protective film, preventing metal-to-metal contact and resisting abrasion under heavy shock loads.
A: They contain extreme pressure (EP) additives and high base oil viscosity to form a resilient protective film, preventing metal-to-metal contact and resisting abrasion under heavy shock loads.
Q: Can heavy-duty bearings really reduce maintenance costs?
A: Yes. By extending service life up to five times and reducing relubrication frequency, they significantly lower non-planned downtime, labor costs, and replacement expenses.
A: Yes. By extending service life up to five times and reducing relubrication frequency, they significantly lower non-planned downtime, labor costs, and replacement expenses.
Q: How do these bearings handle severe misalignment?
A: Spherical roller bearings feature curved outer ring raceways that allow continuous self-alignment, accommodating shaft deflections and structural movements without accelerating wear.
A: Spherical roller bearings feature curved outer ring raceways that allow continuous self-alignment, accommodating shaft deflections and structural movements without accelerating wear.
Q: What role does ultra-clean steel play in bearing longevity?
A: It maximizes internal material purity and fatigue strength, allowing the bearing to safely handle higher dynamic loads and significantly extending its operational lifespan.
A: It maximizes internal material purity and fatigue strength, allowing the bearing to safely handle higher dynamic loads and significantly extending its operational lifespan.
Post time: Sep-14-2026