

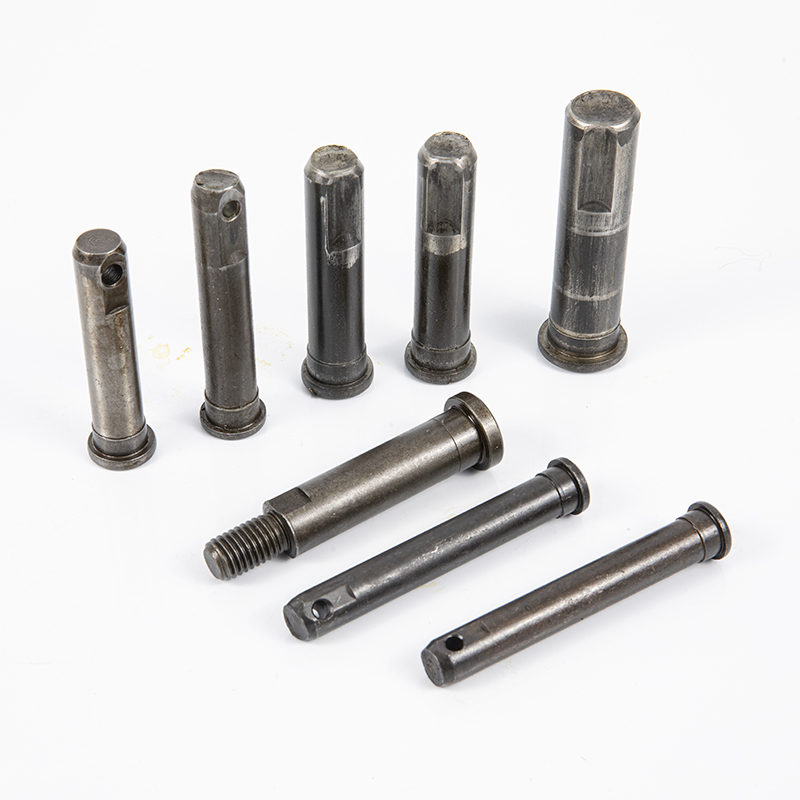
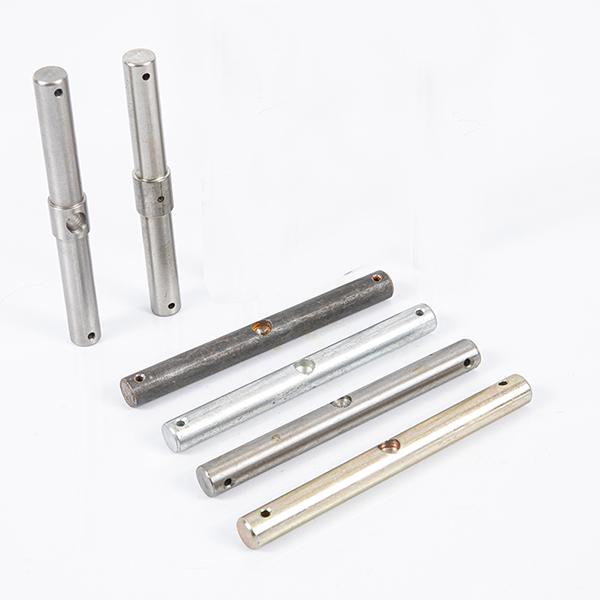
A roller chain pin is the most heavily loaded component in a chain drive. The pin transfers the shear load between the inner and outer link plates, takes the bending load every time the chain articulates around a sprocket, and wears against the bushing at every cycle. The chain pin is also the smallest component, with a diameter typically 3–20 mm depending on the chain size, and the heat treatment of that small component determines whether the chain runs for the published 5–10 year service life or fails in the first 18 months.
This article is written for the procurement engineer, the maintenance manager, and the design lead at an industrial machinery OEM that is specifying a heat-treated roller chain pin for a new machine or a replacement chain. The frameworks below draw on the chain-pin and roller chain parts program at Juding, where the two heat-treatment processes are run on the same pin format and the per-piece cost differential is published in the technical datasheet. The same frameworks apply to any industrial chain pin in the 3–30 mm diameter range, from A-series simplex to heavy-duty conveyor chain.
Why the Heat Treatment Choice Is the Single Most Important Pin Specification
A chain pin is a small part with three jobs, and the heat treatment is the part of the spec that makes the pin capable of doing all three at once. The shear load is the static load the pin carries between the inner and outer link plates at a given chain tension; the bending load is the dynamic load the pin takes every time the chain articulates around a sprocket; the wear load is the surface load the pin takes against the bushing at every articulation. A pin that is too soft fails by wear and by bending fatigue; a pin that is too hard fails by brittle fracture. The heat treatment is what balances the two failure modes.
Three numbers define the pin’s heat treatment. First, the surface hardness, typically expressed in HRC (Rockwell C) or HV (Vickers). The surface hardness is the primary driver of wear life: a pin at 60 HRC lasts roughly 4× the wear life of a pin at 45 HRC, all other things being equal. Second, the core hardness, which determines the pin’s toughness and bending-fatigue resistance. A pin with a hard surface and a soft core (case hardening) is tough enough to absorb a bending shock without cracking; a pin with uniform hardness through the cross-section (through hardening) is stiffer and carries a higher static shear load but is more brittle in bending. Third, the case depth (for case-hardened pins), which is the depth of the hard layer below the surface. A case depth that is too shallow wears through and exposes the soft core; a case depth that is too deep adds cost without a wear-life benefit.
Because the three numbers interact, so the heat treatment spec for a chain pin is a single design choice, not three independent numbers. A pin specified only by surface hardness is a pin that has been designed to fail in a specific way that the spec does not document. The procurement team that asks for the process, the case depth, the surface hardness, the core hardness, and the dimensional tolerance is the procurement team that has a defensible spec sheet; the procurement team that asks for “hardened pin” is the procurement team that has a catalogue page.
The Two Processes Compared: Through Hardening vs Case Hardening
The two industrial-standard heat-treatment processes for chain pins are through hardening (also called quench-and-temper) and case hardening (subdivided into carburizing and induction hardening). They look similar in a datasheet and behave very differently in the field. A procurement team that has both in writing is a procurement team that can match the process to the duty cycle.
| Attribute | Through Hardening (Quench-and-Temper) | Case Hardening (Carburizing / Induction) |
|---|---|---|
| Process | Austenitize at 830–880°C, quench in oil or polymer, temper at 400–600°C | Carburize at 880–930°C in carbon-rich atmosphere, quench; or induction heat the surface layer only and quench |
| Base material | Low-carbon alloy steel (e.g. 20CrMnTi, 8620) | Low-carbon steel (e.g. 1018, 1020) or low-carbon alloy (e.g. 20CrMnTi) |
| Surface hardness | 38–45 HRC (uniform) | 58–62 HRC (case) over 28–35 HRC (core) |
| Case depth | N/A (uniform through cross-section) | 0.5–2.0 mm (carburizing) or 0.8–2.5 mm (induction) |
| Distortion risk | Moderate (full-section quench) | Low (carburizing) to moderate (induction) |
| Re-hardenable in field? | Yes (re-quench-and-temper) | No (case is consumed by wear) |
| Best for | High-impact, high-static-load, heavy industrial chain | High-cycle, low-impact, wear-dominated chain |
| Typical applications | Conveyor chain, mining chain, heavy-duty drive chain | Transmission chain, timing chain, precision conveyor chain |
Because the two processes have different hardness profiles, so the chain duty cycle determines which process is on the table. A high-impact, heavy-load chain (a mining conveyor, a steel-mill drive, a heavy-duty crane) takes through hardening because the pin needs the toughness of a uniform cross-section. A high-cycle, low-impact chain (a transmission chain, a packaging line, a precision conveyor) takes case hardening because the pin needs the wear resistance of a hard surface and the toughness of a soft core. The procurement team that picks through hardening for a high-cycle low-impact chain has a pin that wears 3–4× faster than it should; the team that picks case hardening for a high-impact chain has a pin that cracks on the first shock load.
Process Selection by Application
The process selection is a 4-question decision, and the four questions are answered by the chain duty cycle, the chain size, the operating environment, and the maintenance strategy. The right answer for a 40B conveyor chain is not the right answer for an 08B transmission chain, and the procurement team that picks the same process for both is the procurement team with a maintenance problem on one of them.
Three process-by-application rules are the working default. First, a 40B to 80B conveyor chain (mining, cement, steel-mill, heavy bulk handling) takes through hardening, with a low-carbon alloy steel pin (20CrMnTi or 8620) and a 40–45 HRC target. The chain takes heavy static loads, shock loads at start-up, and a high-cycle count; the pin needs toughness at the centre. Second, an 08B to 24B transmission chain (general industrial, packaging, machine tool, light conveyor) takes case hardening, with a 1018 or 1020 pin or a 20CrMnTi pin, and a 58–62 HRC case over a 28–35 HRC core. The chain takes high cycle counts at moderate load; the pin needs wear resistance at the surface. Third, a precision timing chain or high-speed transmission chain (automotive engine, packaging indexing, machine tool spindle) takes induction case hardening, with a 0.8–1.5 mm case depth and a 60–62 HRC surface. The chain runs at high speed and high cycle count; the pin needs the tightest dimensional control and the highest surface hardness.
The operating environment is part of the process choice. A chain that runs in a clean, dry, indoor environment (a packaging line, a machine tool, an automotive assembly) takes case hardening with a 58–60 HRC surface; the wear is from articulation, not from contamination, and the case depth can be the standard 0.5–1.0 mm. A chain that runs in a dusty, wet, or corrosive environment (a mining conveyor, a wash-down food line, a marine drive) takes through hardening with a 38–42 HRC through-section; the wear is from contamination and corrosion, and the uniform hardness means the pin survives the surface damage that would expose a soft core in a case-hardened pin.
What Goes Wrong: Three Common Heat-Treatment Failures
Three failure modes account for the majority of chain-pin warranty claims. None of them are catastrophic; all three are preventable with a documented process specification and a documented incoming-QC protocol.
- Case wear-through on a case-hardened pin. The case is the hard layer; once it wears through, the soft core is exposed and the pin wears 5–10× faster than the published rate. A case that is too shallow (under 0.5 mm for a 5 mm pin) wears through in 3–6 months in a high-cycle duty. Prevention: specify a minimum case depth in writing (typically 0.8 mm for a 5 mm pin, scaling with pin diameter) and audit the case depth on a sample of incoming pins with a Vickers microhardness traverse.
- Quench cracking on a through-hardened pin. The quench is the most violent part of the through-hardening process, and a quench that is too aggressive (water instead of oil, oil that is too cold, or a quench delay that is too long) can crack the pin before it ever ships. Prevention: specify the quench medium, the quench temperature, and the maximum delay between the austenitize and the quench in writing; audit the quench bath temperature on every batch.
- Case-core debond on a carburized pin. A case that is not properly fused to the core (a decarburized layer at the interface) spalls under shock load, exposing the soft core and accelerating the wear. The decarburization happens at the austenitize step if the carbon potential of the atmosphere is too low. Prevention: specify the carbon potential of the carburizing atmosphere and audit the case-core interface with a metallographic cross-section on a sample of every batch.
Procurement Checklist: Eight Questions to Ask the Chain Pin Supplier
Eight questions, in order, that resolve the heat-treatment spec for a chain pin order. Answer them in writing, attach the answers to the supplier brief, and use them as the incoming-QC checklist on receipt.
- What is the chain size and the duty cycle? 08B–24B, low-impact, high-cycle = case hardening. 40B–80B, high-impact, high-load = through hardening. The duty cycle is the first gating constraint.
- What is the base material? 1018 / 1020 for case hardening; 20CrMnTi / 8620 for through hardening or higher-grade case hardening. The material is the second constraint.
- What is the heat-treatment process? Through hardening (quench-and-temper) or case hardening (carburizing or induction). The process is the third constraint.
- What is the surface hardness? 38–45 HRC for through hardening; 58–62 HRC for case hardening. The surface hardness is the fourth constraint.
- What is the core hardness? N/A for through hardening; 28–35 HRC for case hardening. The core hardness is the fifth constraint.
- What is the case depth? 0.5–2.0 mm (carburizing) or 0.8–2.5 mm (induction), scaling with pin diameter. The case depth is the sixth constraint.
- What is the dimensional tolerance? h6 or h7 on the pin diameter, depending on the chain size; the tolerance is the seventh constraint.
- What is the surface finish? Ra 0.4–0.8 µm on the pin bearing surface; a smoother finish than that does not add wear life and a rougher finish accelerates the wear. The surface finish is the eighth constraint.
The eight questions above are the spec template any procurement team should be running against every chain-pin order. The supplier that answers all eight with a published datasheet, a metallographic case-depth report from a recent batch, and a documented incoming-QC protocol is the supplier that will deliver a 5–10 year service life. The supplier that answers two of them is a trading company, and the procurement team is better off walking away before the order ships.
Frequently Asked Questions
What is the difference between through hardening and case hardening?
Through hardening (quench-and-temper) gives a uniform hardness across the entire pin cross-section, typically 38–45 HRC for a low-carbon alloy steel pin. Case hardening (carburizing or induction hardening) gives a hard case (58–62 HRC) over a tough core (28–35 HRC), with the case typically 0.5–2.0 mm deep. Through hardening is for high-impact, heavy-load chains; case hardening is for high-cycle, wear-dominated chains.
What is induction hardening vs carburizing for chain pins?
Both are case-hardening processes. Induction hardening uses an induction coil to heat the pin surface only, then quenches; the case depth is typically 0.8–2.5 mm and the cycle time is short (seconds per pin). Carburizing uses a carbon-rich atmosphere at 880–930°C to diffuse carbon into the pin surface, then quenches; the case depth is typically 0.5–2.0 mm and the cycle time is long (hours). Induction is the right answer for a high-volume, tight-tolerance pin; carburizing is the right answer for a heavier pin with a deeper case.
What is the typical case depth for a 5 mm chain pin?
For a 5 mm pin, the case depth is typically 0.5–1.0 mm for a transmission chain and 1.0–1.5 mm for a heavy-duty chain. A case depth under 0.5 mm on a 5 mm pin wears through in 3–6 months in a high-cycle duty; a case depth over 1.5 mm adds cost without a wear-life benefit. The 0.8 mm target is the working default.
How is case depth measured on a chain pin?
Case depth is measured by a Vickers microhardness traverse on a metallographic cross-section: the pin is cut, mounted, polished, etched, and indented at 50µm intervals from the surface to the core. The case depth is the distance from the surface to the point where the hardness falls to 50 HRC (for case-hardened pins) or to the core-hardness value (whichever is higher). A supplier that cannot produce a Vickers traverse report is a supplier that cannot document the case depth.
Can a chain pin be re-heat-treated in the field?
A through-hardened pin can be re-hardened by re-quenching, but the dimensional change is uncontrolled and the pin will need re-grinding to restore the tolerance. A case-hardened pin cannot be re-hardened in the field; once the case is consumed by wear, the pin is scrap. The procurement team that is buying a chain for a remote site should stock 2× the in-service pin count and plan for a 2-year replacement cycle, not a 5-year replacement cycle.
What is the difference between a press-fit pin and a rivet pin?
A press-fit pin is pressed into the chain during OEM assembly and is held in place by interference fit. A rivet pin has a head formed after the heat treatment and is held in place by the head and a flared end. A press-fit pin is the right answer for an OEM assembly; a rivet pin is the right answer for an in-field repair. Both pins take the same heat treatment; the difference is the assembly process.
What is the standard chain-pin material for an industrial chain?
20CrMnTi is the working default for an industrial chain pin in the Chinese supply chain; 8620 and 4140 are the working defaults in the US and European supply chains. 1018 and 1020 are the working defaults for case-hardened pins. A pin specified without a material grade is a pin specified for failure.
How do I verify a chain-pin supplier’s heat-treatment claim?
Request three documents in writing: a published datasheet with the surface hardness, core hardness, case depth, and dimensional tolerance; a metallographic case-depth report from a recent production batch; and an incoming-QC protocol that the supplier runs on every shipment. A supplier that can produce all three in 5–10 working days is a supplier that has the documentation practices that an industrial chain program requires.
Where to Go From Here
If you are specifying a heat-treated chain pin for a new industrial machine or a replacement chain program, the next step is to share the eight-question procurement checklist with the supplier and request a written response with the process spec, the case-depth report, and the incoming-QC protocol. The roller chain parts product line shows the chain size and pin format range supported by the Juding program. The roller chain pin product page has the heat-treatment process spec, the case-depth report, and the dimensional tolerance for the standard pin formats. For a custom pin format with a brand-specified heat-treatment process, the rivet pin for assembled roller chain program covers the in-field repair use case, and the Juding engineering team can quote a custom heat-treatment spec in 5–10 working days from a confirmed spec.
Send the eight-question procurement checklist to your shortlist and request a metallographic case-depth report from a recent production batch. A serious supplier answers in 5–10 working days; a trading company cannot answer the case-depth question. The Juding engineering team is the entry point for the heat-treatment conversation.
Post time: Oct-15-2026